
NewsDetails
Can We Order Custom Colors and Surface Finishes?
author:Hongxing time:2026-10-20 14:40:41 Click:0
The Short Answer
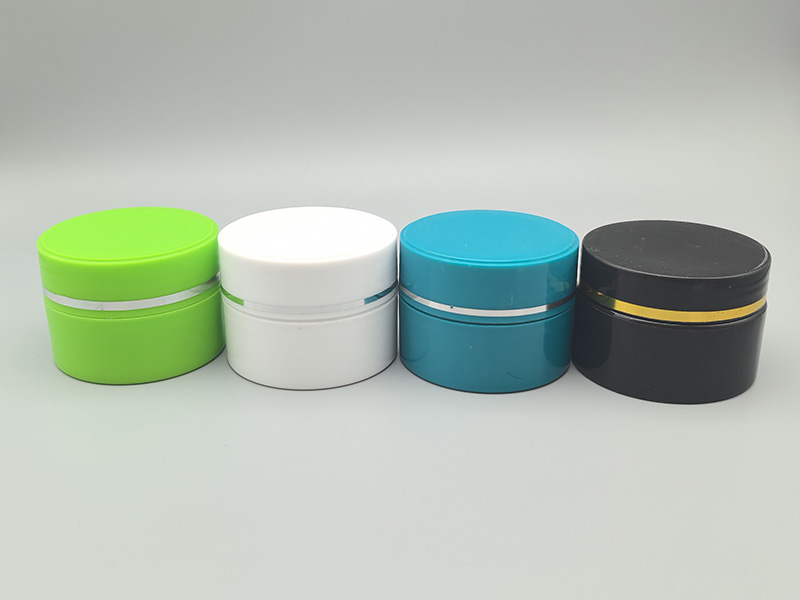
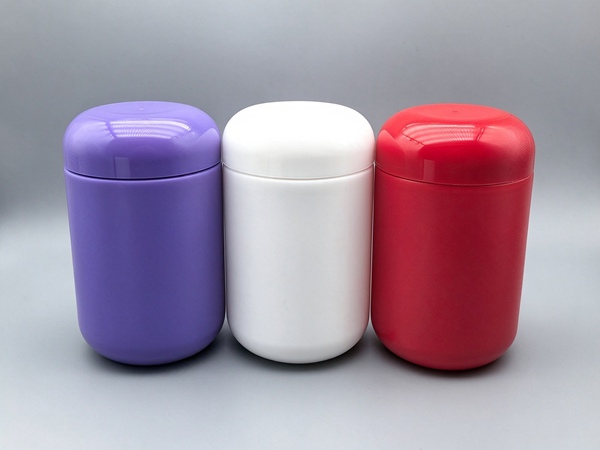
Yes. Color is normally produced by dosing a masterbatch into the resin, and finish is produced either by the mold surface or by a post-molding treatment. Custom colors require a color match and a minimum batch of masterbatch; finishes such as matte, frosted or soft-touch may require a different mold surface, a secondary process or both. The practical constraints are minimum quantities and the fact that a color approved on a flat chip may look different on a curved, glossy part.
How Custom Color Is Produced
Pigment is supplied as masterbatch, a concentrated dispersion in a carrier resin, and dosed at a fixed percentage during molding. Achieving a specific color therefore involves matching the pigment formulation, then confirming that the color survives the melt temperature and shear of the process. Some organic pigments shift hue at high temperature, and some inorganic pigments lose opacity when dispersed poorly. For critical colors, a pre-compounded resin removes dosing variation and gives the most repeatable result, at a higher material cost.
Surface Finishes
A glossy finish comes from a polished mold and is the default. A matte finish can be produced by etching the mold surface, which is durable but permanent, or by a post-molding coating, which is flexible but adds a process and a compatibility question. Frosted effects are achieved either by etching or by a specially formulated resin. Soft-touch coatings give a rubbery feel and are popular on premium packs, but they are vulnerable to solvents and abrasion and should be tested with the product and with handling in mind. Each finish changes how the same color appears, because surface texture alters light reflection.
What Drives Cost and Minimums
Custom color adds a masterbatch development charge and a minimum purchase of masterbatch, which is usually expressed in kilograms and translates into a minimum number of parts. A custom mold surface adds tooling work. Post-molding coatings add a process step and often a minimum run per color. Where the quantity is modest, a stock color with a printed or labeled design usually delivers a distinctive result at a fraction of the cost, and the saved budget is better spent on structure or decoration.
Avoiding Approval Problems
- Approve a molded part, not a printed color chip.
- Specify the resin and the finish together, since they interact.
- Check the color under at least two light sources.
- Ask for the color to be measured numerically, not judged by eye alone.
- Confirm that the finish survives an abrasion and solvent rub test.
- Clarify whether the price includes masterbatch development.
- Agree a tolerance for batch-to-batch variation in writing.
Matching Colors Across Components
Bottle, cap, collar and dispenser are often molded from different resins, and the same pigment produces different results in each. PP, ABS and PET differ in base color, in how they scatter light and in how much pigment they can carry, so a single reference will not translate directly. The usual solution is to approve each component against the same master under the same lighting, and to accept that absolute identity is unrealistic while close visual harmony is achievable. Where a cap and body must match precisely, using the same resin family for both is the most reliable route.
Finishes and the Perception of Value
Finish changes perceived quality more than color does. A matte surface reduces visible fingerprints and scratches, which matters for a product handled daily; a gloss surface reads as clean and clinical but shows every mark. Soft-touch coatings feel premium and hide mold imperfections, but they collect lint and are difficult to clean, which is a poor match for products used in bathrooms. Frosted effects sit between the two and are popular because they suggests glass without its weight. Each choice should be tested with real handling rather than judged from a sample under studio light.
Lead time is affected by color as well as cost. A custom color requires pigment matching, a masterbatch batch to be produced, and usually a color trial before production, which can add one to three weeks. Where a launch date is fixed, choosing a color from an existing masterbatch range and using decoration to create differentiation is often the difference between shipping on time and shipping late.
Conclusion
Custom color and finish are routine, but they are process decisions rather than design decisions. Masterbatch dosing, mold surface and coating all influence the final appearance, and the same color can look different on each. Approving a molded part and testing the finish against the product removes most of the risk, and a stock color with strong decoration remains the pragmatic choice for smaller volumes.
References
- ISO 105-A02:1993, Textiles — Tests for colour fastness — Grey scale for assessing change in colour.
- ASTM D2244-23, Standard Practice for Calculation of Color Tolerances and Color Differences.
- ASTM D523-14(2018), Standard Test Method for Specular Gloss.
- ISO 2409:2020, Paints and varnishes — Cross-cut test.
- ISO 9001:2015, Quality management systems — Requirements.
- EU Regulation No 10/2011 on plastic materials and articles intended to come into contact with food.
 Recommended Products
 Contact us
—— Contact:Mr. Liu
—— Tel:+86 15630715521
—— Email:1324265984@qq.com
—— Url:https://www.hongxingpackaging.com
—— Address:Dusheng Town, Cang County, Cangzhou City, Hebei Province, China