
NewsDetails
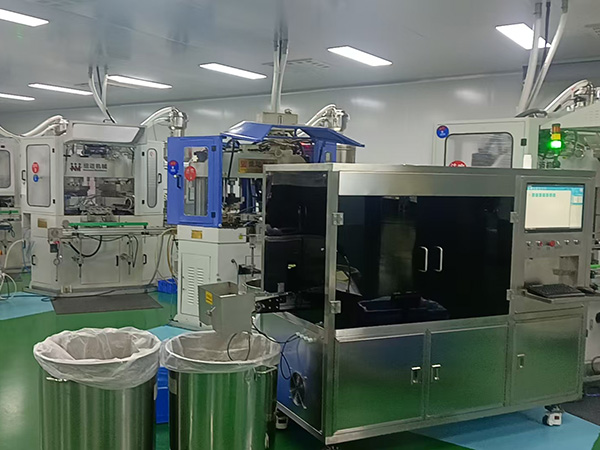
Filling Line Compatibility: Capping Torque, Changeover and Line Efficiency
author:Hongxing time:2026-10-20 14:36:12 Click:0
Abstract
Packaging that looks good in a sample box can stop a filling line. Neck ovality, unstable bases, cap geometry that does not suit the chute, and closures that need a different torque all translate into downtime that is rarely attributed to the pack. This article describes the line-side characteristics that determine whether a container runs smoothly at production speed, and the design changes that fix the most common problems.
Container Stability on the Line
A bottle or jar must travel on conveyors without tipping, and it must sit squarely under the filler and the capper. Tall narrow bottles with a small base are the usual culprits: they vibrate as the conveyor moves, lean against guide rails and jam at transfers. Base design matters more than overall proportions, and a recessed base with a defined standing ring gives better stability than a flat bottom that rocks on an imperfect surface. Lightweighting makes this harder, because the same geometry with less material is more flexible; the practical limit is reached when the pack deforms under the filler nozzle or when the base creeps during storage.
Neck Dimensional Control
Fillers locate the bottle by the neck, and cappers grip it by the same feature. Neck inner diameter, thread position and ovality must therefore be controlled more tightly than the rest of the container. An oval neck causes the cap to cross-thread, which produces a leak that appears only after the pack has been shipped. Neck height variation shifts the capping head's reference point, so torque applied by a fixed head varies from pack to pack. Specifying neck dimensions with tolerances and checking them with plug gauges at receiving inspection is cheaper than discovering the problem on a running line.
Capping Torque Consistency
Torque consistency depends on three factors: the capping head's setting, the friction between cap and neck, and the closure's internal geometry. Lubricity varies between resin lots, so a closure that caps at the target torque in one batch may run high in the next. The practical control is to measure removal torque on samples at the start, middle and end of each run and to adjust the head rather than to widen the specification. Magnetic clutches are common and are convenient, but they drift; a calibration check at each shift prevents a slow drift from producing a pallet of over-torqued packs that consumers cannot open.
Changeover and Format Flexibility
Changeover time is a hidden cost of packaging variety. Packs that share neck dimensions, cap diameters and heights allow the line to switch with minimal adjustment, while a new format may require different change parts, a new chute and a new capping head. Brands planning a family of products benefit from selecting a small number of neck standards across the range. Where changeover is unavoidable, designing the pack so that change parts are few and accessible shortens the downtime, and documenting the settings for each SKU removes the trial-and-error that otherwise consumes the first hour of every run.
Line Trial Checklist
- Run at target speed, not at half speed, for at least thirty minutes.
- Record jam locations and frequencies, not just total downtime.
- Measure torque on at least thirty packs across the run.
- Check fill weight variation at the start and end of the run.
- Inspect for scuffing and stress marks caused by guide rails.
- Verify cap orientation at the sorter and any missed caps.
- Confirm changeover time with a timed trial, not an estimate.
- Leak-test packs from the first and last ten minutes of the run.
Common Line Defects and Their Packaging Causes
Scuffing on the shoulder usually means guide rails are set too tight for the container's diameter tolerance. Capping marks on the cap skirt indicate the chuck is gripping too low or with excessive force. Incomplete caps at the sorter point to a cap that is too light or has a geometry that allows it to nest. Product on the thread after filling often comes from a nozzle that is too large for the neck, causing the stream to splash back. None of these defects is mysterious once the mechanism is understood, and each has a packaging-side remedy as well as a machine-side one. Recording defects with photographs and the machine settings in force at the time builds a reference that shortens every subsequent troubleshooting session.
Conclusion
Line compatibility is a design property expressed in geometry and tolerance. Stable bases, controlled necks, consistent friction and shared neck standards determine whether a pack runs at speed. A structured line trial that records jam locations and torque data turns a vague complaint about "difficult packaging" into a specific, correctable specification change.
References
- ISO 2859-1:1999, Sampling procedures for inspection by attributes.
- ISO 9001:2015, Quality management systems — Requirements.
- ASTM D3474-20, Standard Practice for Calibration and Use of Torque Meters.
- ISO 8317:2015, Child-resistant packaging — Requirements and testing procedures.
- ASTM D4169-22, Standard Practice for Performance Testing of Shipping Containers and Systems.
- USP <671>, Containers — Performance Testing.
 Recommended Products
 Contact us
—— Contact:Mr. Liu
—— Tel:+86 15630715521
—— Email:1324265984@qq.com
—— Url:https://www.hongxingpackaging.com
—— Address:Dusheng Town, Cang County, Cangzhou City, Hebei Province, China